Language:


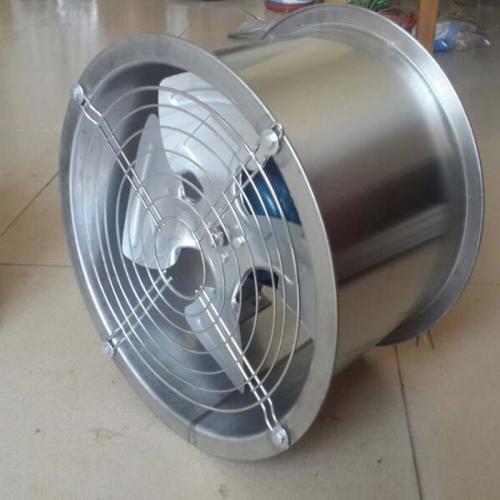
Ceramic composite relies on hard alumina to resist abrasive cutting; hardness is far above a hardfaced deposit, but the material is brittle and sensitive to how it is fixed. The design problem is not the ceramic itself but the anchoring and the joints that keep blocks from detaching.
Liners suit low velocity, blunt angle wear zones, while high velocity impeller areas usually use hardfacing or spraying, so the two are often combined.
| Location | Process | Typical figure |
| Volute inner wall | Alumina ceramic composite liner | Alumina content 92%-95% |
| Inlet cone | Ceramic tiles or composite liner | Hardness typically HRA 88-92 |
| Impeller front plate | Local ceramic composite | Applied to the wear pattern |
| Duct bends | Replaceable ceramic liner | Severe blunt angle wear zone |
| Joints and edges | Resin or dedicated adhesive sealing | Prevents peeling from the edge |
| Location | Process | Typical figure |
| Block layout | Blocks shaped to the flow path with expansion gaps | Releases thermal and vibration stress |
| Anchoring | Welded anchors combined with adhesive bonding | Improves overall reliability |
| Adhesive control | Controlled bond line thickness and curing | Ensures bond strength |
| Edge protection | Corner strip or retaining batten at edges | Stops high velocity flow lifting the edge |
| Inspection | Tap testing for voids at intervals | Finds detachment risk early |
Applications include aggregate crushing, cement grinding, foundry sand handling, ceramic and glass polishing and mineral powder conveying.
Where the medium contains fluorides the glass phase of the ceramic is attacked, so a ceramic liner alone is not suitable and the material combination has to be reconsidered.
Liners should be designed as replaceable parts so that blocks can be renewed by wear measurement without damaging the main structure.
| Standard | Title | Purpose |
| GB/T 4340.1 | Metallic materials - Vickers hardness test - Part 1 | Coating and hardened layer hardness |
| ASTM G65 | Standard test method for measuring abrasion using the dry sand/rubber wheel apparatus | Relative abrasive wear resistance |
| GB/T 24186 | High strength abrasion resistant steel plates for construction machinery | Wear plate material acceptance |
| GB/T 1236 | Industrial fans - Performance testing using standardized airways | Air flow, pressure and efficiency testing |
| GB/T 9239.1 / ISO 21940-11 | Mechanical vibration - Balance quality requirements for rigid rotors | Impeller balancing grade |
Please provide particle size, dust concentration, inlet velocity and medium temperature. Size and motor power are calculated for the actual duty.
Detachment usually starts at joints and edges. Block layout with expansion gaps, welded anchors combined with adhesive, edge protection and periodic tap testing keep the risk within acceptable limits.
For pure abrasive wear, alumina ceramic is harder and lasts longer, but it does not tolerate impact or fluoride bearing media and performs worse than hardfacing under coarse particle impact or strong vibration. Practical schemes often combine both.
Yes, that is the advantage of composite lining. Replacement by wear measurement keeps the main structure intact, and common sizes should be included in the spare parts list at the design stage.
Related pages: Wear-resistant fan range Wear-resistant centrifugal fan Dust collection and wear protection
Contact: Lee
Phone: 13793313126
Tel: 0533-6820280
Email: chuanyi99@126.com
Add: Wujia Industrial Park, Nanjiao Town, Zhoucun District, Zibo City, Shandong Province, China