Language:



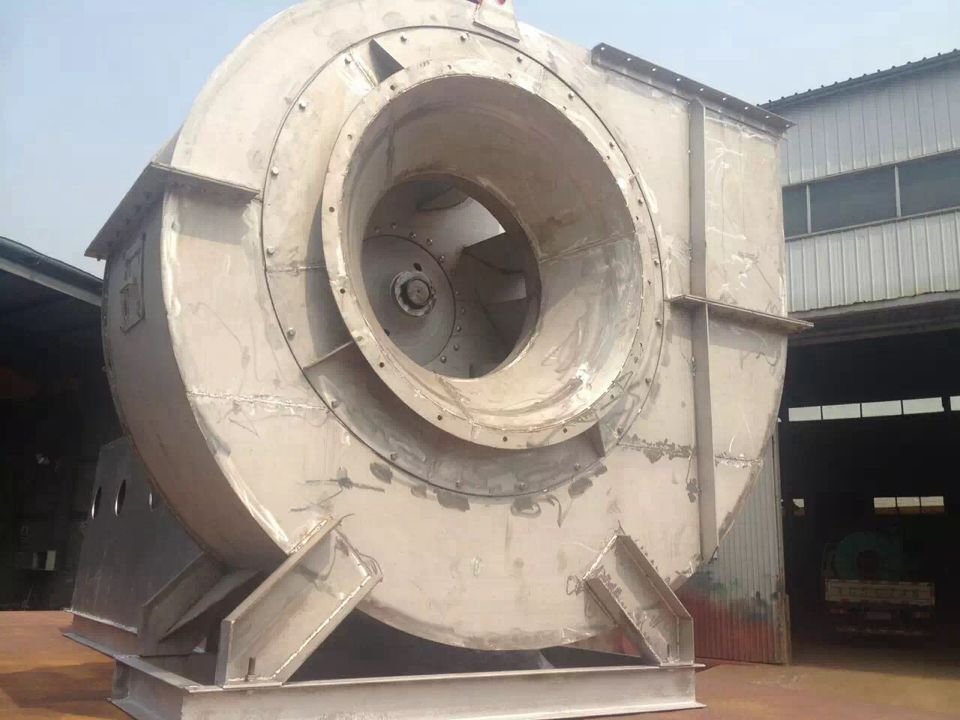
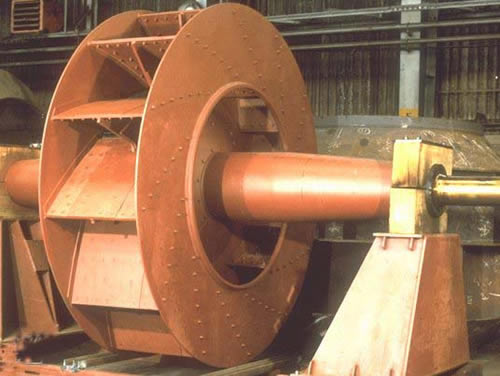
600 C is firmly in heat resistant steel territory and usually comes with heavily dust laden gas. The main material is 12Cr1MoV, the bearing assembly is water cooled and the casing is lined with ceramic fibre, so temperature, wear and sealing are solved together.
Pearlitic heat resistant steel provides the creep and oxidation performance needed at this level.
| Location | Material / process | Basis |
| Impeller and casing | 12Cr1MoV (GB/T 5310) | Good creep and oxidation resistance at 600 C |
| Welding consumables | Heat resistant electrodes (GB/T 5117) | Maintains weld strength at temperature |
| Bearing assembly | Water cooled bearing housing | Removes bearing heat positively |
| Insulation | 50 mm ceramic fibre lining plus external insulation | Lowers metal wall temperature |
| Wear zones | Hardfacing on blades and liner plates | Combines temperature and abrasion resistance |
| Location | Material / process | Basis |
| Water cooled bearing housing | Jacket with circulating water and temperature monitoring | Keeps bearings within their limit |
| Expansion joints | Bellows joints in hot ducts (GB/T 12777) | Absorbs thermal displacement |
| Combined sealing | Labyrinth seal with graphite packing | Limits hot gas leakage |
| Welding procedure qualification | Qualified procedure with test coupon | Prevents weld cracking in service |
| Ceramic fibre anchoring | Anchors fixed to the casing | Stops the lining from collapsing |
Typical duties are power plant boiler induced draft, cement kiln tail gas, coke oven gas and carbon rotary kilns.
Dust load is often high at this level, so wear resistance and temperature resistance have to be designed together.
Where dust load is high, a pre-collector ahead of the fan is recommended and the separation efficiency should be written into the technical agreement.
| Standard | Title | Purpose |
| GB/T 5117 | Covered electrodes for manual metal arc welding of non-alloy and fine grain steels | Welding consumable matching |
| GB/T 1236 | Industrial fans - Performance testing using standardized airways | Air flow, pressure and efficiency testing |
| GB/T 12777 | General specification for metal bellows expansion joints | Expansion compensation for hot ducts and casing |
| GB/T 9239.1 / ISO 21940-11 | Mechanical vibration - Balance quality requirements for rigid rotors | Impeller balancing grade |
| GB/T 10178 | Industrial fans - Performance testing in situ | On-site performance verification |
Please provide medium temperature, gas composition, dust load and air flow. Fan size and motor power are calculated for the actual duty.
It adds cooling water management, but without water or forced cooling the bearing life at 600 C cannot normally be guaranteed. Water temperature, flow monitoring and a low flow alarm are recommended.
For dust laden gas, yes. Hardfacing is normally applied to the wear prone areas and the rotor is re-balanced to G6.3 or tighter afterwards.
Pearlitic heat resistant steels such as 12Cr1MoV are prone to hardening and cracking in the heat affected zone, and the risk grows during long term hot operation, so consumables, preheat and post weld treatment follow a written procedure.
Related pages:
Contact: Lee
Phone: 13793313126
Tel: 0533-6820280
Email: chuanyi99@126.com
Add: Wujia Industrial Park, Nanjiao Town, Zhoucun District, Zibo City, Shandong Province, China